Wetting Issues and Surface Tension Requirements for Aluminum Die-Casting Release Agents
Introduction
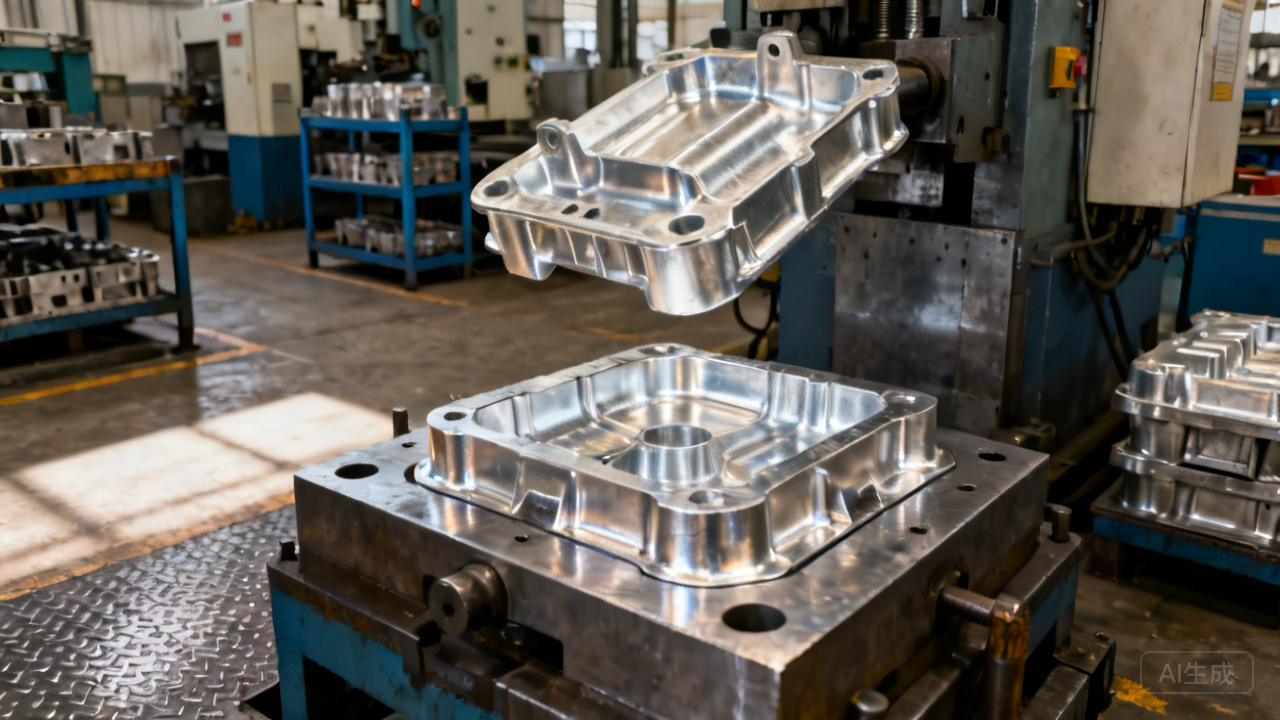
In aluminum die-casting production, uneven spraying of release agents often leads to die sticking and surface defects on castings. The root cause is insufficient wetting of the release agent, which fails to form a uniform film on the mold surface. Controlling surface tension at an appropriate level is the key to resolving this issue.
Common manifestations and hazards of insufficient wetting of aluminum die-casting release agents
- Manifestations: The release agent retracts into bead-like droplets after spraying and fails to spread; local demolding difficulty occurs on castings, with flow marks and porosity on the surface.
- Hazards: Shortens mold service life, increases reject rate, and reduces production efficiency. The root cause is excessive interfacial tension between the release agent and the mold surface, preventing effective reduction of the contact angle.
Key role of surface tension in release agent formulations and parameter requirements
Static surface tension vs. dynamic surface tension
- Static surface tension: Determines the final spreading ability of the release agent on the mold surface.
- Dynamic surface tension: Affects the rapid spreading of droplets during the spraying process, and is particularly critical for high-pressure spraying processes.
Specific surface tension parameters for aluminum die-casting processes
- Recommended range: The static surface tension of a 0.1% aqueous solution should be ≤28 dyn/cm; the dynamic surface tension (10 Hz) is recommended to be ≤32 dyn/cm.
- Empirical values: When surface tension is below 26 dyn/cm, wetting performance is significantly improved; when above 30 dyn/cm, shrinkage cavities and wetting blind spots are prone to occur.
Optimizing wettability through additive selection: Toynol® product solutions
High-efficiency acetylenic diol wetting agents
- Toynol® Superwet-320: The static surface tension of a 0.1% aqueous solution is only 26.2 dyn/cm, with low-foam performance; suitable for high-pressure spraying applications.
- Toynol® FS-204BC (and the same series FS-204/FS-204E): Excellent dynamic surface tension reduction capability, with foam-inhibiting function to avoid microbubbles during high-speed spraying.
Foam-control wetting agents (combining foam management)
- Toynol® FS-620: Static surface tension 33.2 dyn/cm (0.1%), dynamic surface tension 34.3 dyn/cm; suitable for formulations with low foam tolerance.
- Toynol® Foamic 024: Silicone-free and mineral oil-free, works synergistically with wetting agents to help reduce shrinkage cavities; recommended dosage 0.2%-1.0%.
Dispersing and stabilizing additives
- Toynol® ADS-20: When the formulation contains release agent powders (e.g., wax powder), it assists dispersion and improves uniformity.
Practical recommendations and dosage references
- Recommended dosage: Wetting agents are typically used at 0.3%-0.5% of the total release agent formulation.
- Compatibility testing: Quick screening approach: apply a 0.1% additive aqueous solution onto a mold substrate (e.g., H13 steel) and measure the contact angle; below 20° is considered acceptable.
- Example combined solution: Superwet-320 at 0.4% + Foamic 024 at 0.3% simultaneously addresses wetting and foam issues.
Conclusion
The wetting performance of aluminum die-casting release agents directly affects product yield. Prioritizing acetylenic diol gemini-type low-surface-tension additives (such as Toynol® Superwet-320 and the FS-204 series) and maintaining surface tension within the 26-30 dyn/cm range provides a reliable pathway to building high-performance release agent formulations.